
未分类

wrinkle defects

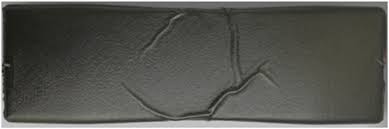
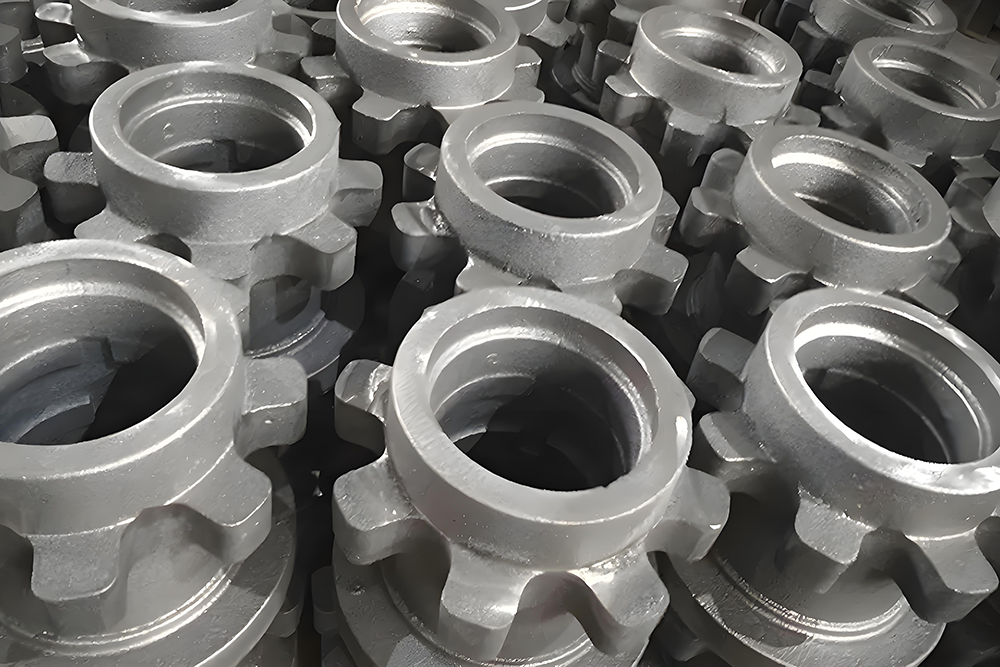
Formation and prevention of wrinkle defects on the surface of ductile iron parts in lost foam casting

Wrinkle defects often appear at the last place where the molten metal flows or the “cold end” of the liquid flow, generally appearing at the top of the casting, vertical sidewalls or dead corners. The surface of this type of defect is often covered with light and shiny carbon flakes, and the depression of the […]
Formation and prevention of wrinkle defects on the surface of ductile iron parts in lost foam casting Leer más »

cast iron parts

Causes and countermeasures of blistering defects on the surface of cast iron parts produced by lost foam

Causes Mold aspect: the gas emission of the mold material is too large, and a large amount of gas is released during pouring. If there is no time to discharge, bubbles will form on the surface of the casting. Uneven density of the mold and poor local gas discharge will also cause bubbles. Coating aspect:

Causes and countermeasures of blistering defects on the surface of cast iron parts produced by lost foam Leer más »

medium carbon steel

Causes and countermeasures of shrinkage and pore defects in medium carbon steel

Causes Solidification shrinkage: The carbon content of medium carbon steel is between 0.25% and 0.60%. When solidifying, the liquid state changes to solid state and the volume shrinks. If the liquid metal is not replenished enough during the solidification process, shrinkage holes will be formed inside or on the surface of the casting. Cooling rate:

Causes and countermeasures of shrinkage and pore defects in medium carbon steel Leer más »

feed wire spheronization process

Introduction to wire feeding spheroidization process

1. Basic principle of wire feeding spheroidization process Wire feeding spheroidization means wrapping a spheroidizer in a steel sheet using a winding device. The steel sheet has specific thickness and width to form a cable-shaped cored wire roll. The wire roll must have suitable strength and a proper filling rate for processing. A wire feeding

Introduction to wire feeding spheroidization process Leer más »

melting deoxidation

Induction furnace cast steel melting deoxidation and refining method

1. Pre-deoxidation Pre-deoxidation time: When the steel material has been completely melted, but the temperature is not high, generally about ≥1550℃, it is the best time for pre-deoxidation. Selection of pre-deoxidizer: Select manganese and silicon with better deoxidation effect and higher residual steel as pre-deoxidizer. Electrolytic manganese and crystalline silicon are used for steel with

Induction furnace cast steel melting deoxidation and refining method Leer más »